My Machine Is Built: Can Another Company Write Its PLC Software?
The mechanics and electrical cabinet are ready, but the PLC program is missing. What an independent programmer needs, how HMI scope is agreed and what commissioning involves.
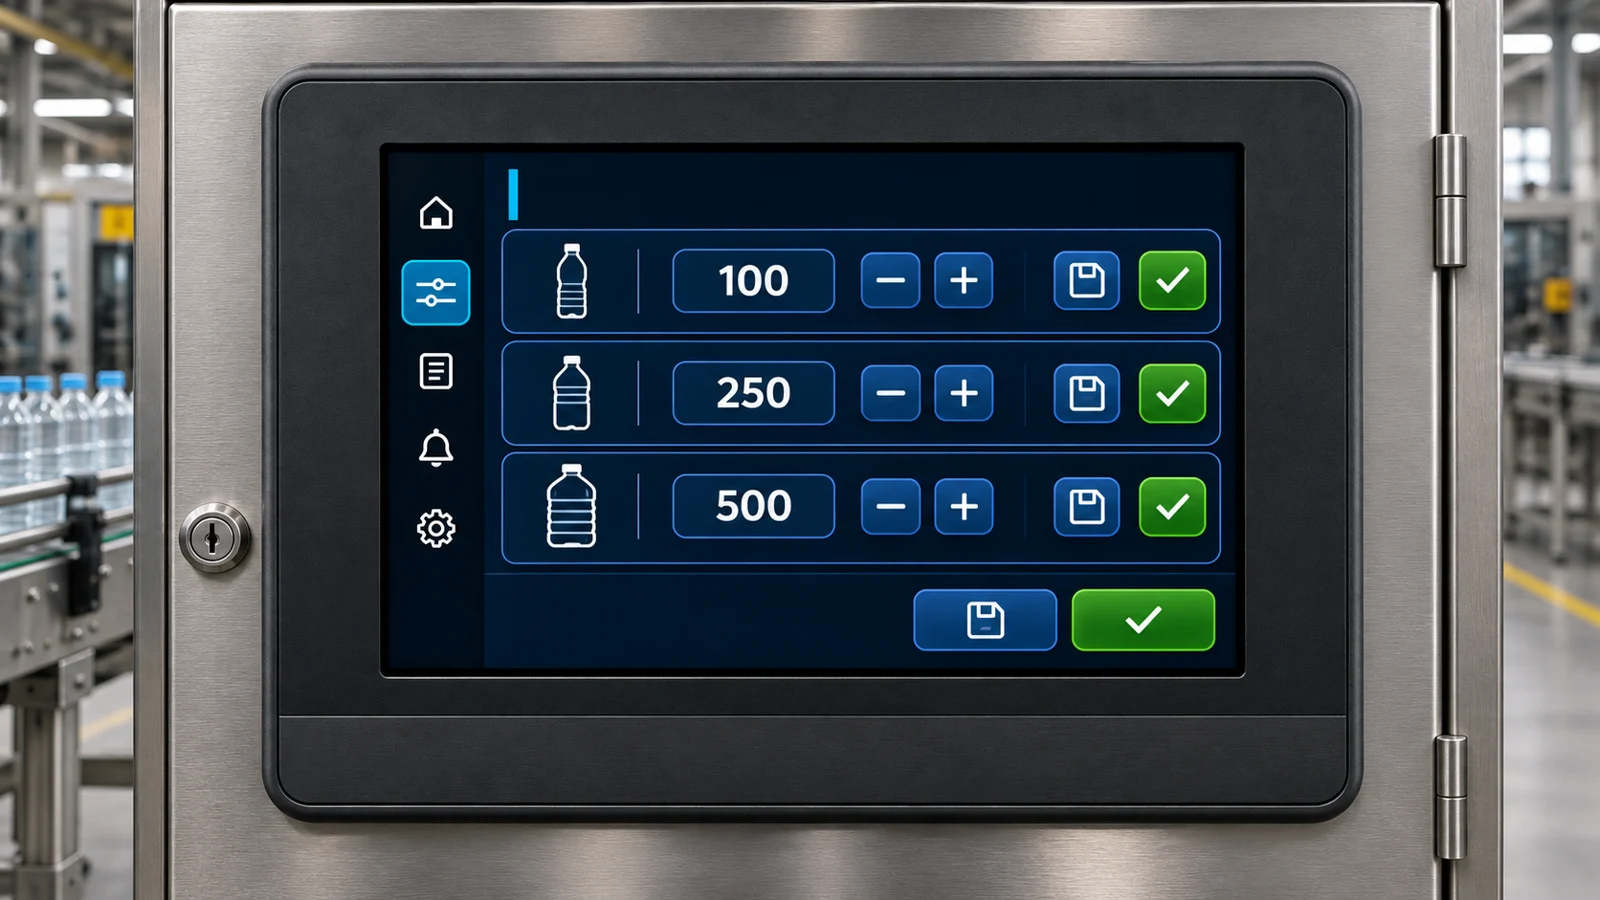
Yes. A new machine built by one manufacturer can have its PLC software developed by an independent automation company. The PLC brand alone is not enough to begin: the operating sequence, electrical drawings, inputs and outputs, drives and operator requirements must be reviewed together.
This article concerns new machinery whose program has not yet been completed. Changing an existing machine also requires checking the available source project, access permissions and recovery options.
Can the mechanical builder and PLC programmer be different companies?
Yes, provided their responsibilities and technical information are coordinated. The mechanical builder explains the intended movements, the electrical team identifies the connected equipment, and the software team defines the operating sequence and checks.
“Make the machine run” needs detail: what happens when a sensor does not respond, product runs out or the operator stops a cycle? These decisions should be written down before testing.
Başakşehir Makine develops PLC software for machines built by other manufacturers as well as its own equipment. This is not limited to filling or packaging machinery. Send the machine information so we can assess the project.
Let’s talk about your machine
If you’d like to talk, leave your name and phone number and we’ll give you a call.
Thank you. We’ll be in touch.
What information is needed?
InformationPurposeExact PLC, HMI and module modelsSoftware, communication and capacity compatibilityElectrical drawings and I/O listIdentify sensors, valves, motors and addressesOperating sequenceDefine normal operation, stops and waiting conditionsDrive and peripheral detailsAgree control and communication methodsRequired screens and settingsSeparate HMI, recipe, alarm and access scopeAcceptance expectationsDefine the tests and delivery conditionsMissing documents can be identified during an initial review. However, undocumented wiring or unknown field devices can require extra investigation; a photograph alone does not establish a firm price or completion time.
How do I describe the sequence without knowing code?
Describe one cycle in ordinary language. For example: a bottle arrives, the conveyor stops, filling starts when the necessary conditions are met, and the next bottle advances when filling finishes.
Then describe exceptions: a missing bottle, delayed sensor, interrupted cycle, power loss or a stop request. The programmer converts these requirements into control logic; the equipment still needs physical verification.
Is HMI programming included automatically?
No. Agree it as part of the scope. Decide which settings operators can change, which alarms need explanations, whether products need recipes and how access is restricted. A few start and stop controls and a complete recipe interface are different projects.

Can the PLC be supplied and programmed?
If a controller has not been chosen, we can assess suitable equipment, supply and programming together. I/O count, signal types, communication, drives and available space influence the choice. Having the required brand in a list does not prove that every CPU model supports the project.
Can everything be completed remotely?
Some development and diagnostics can be carried out remotely with suitable access and an authorised person at the machine. Shipping a controller can help with compatible offline tasks. Neither approach replaces testing actual sensors, actuators, interlocks and the assembled machine.
On-site commissioning may therefore be required. Remote access, responsibilities and downtime are agreed before work begins. See our PLC remote-support guide.
What should commissioning and handover include?
Agree a test plan covering individual functions, the normal cycle, missing signals, stops, restarting and operator settings. Responsibility for machine safety, protective functions and final acceptance must be clear; ordinary PLC logic alone does not establish a safe machine.
Discuss delivery of the editable source project at the beginning. Include the I/O list, basic operating notes, parameter records, known limitations and backup arrangements. Reading data back from a PLC does not always recover the complete commented source project.
PLC backup and recovery checklist
What determines the price?
Movement and sequence complexity, documentation quality, drives, HMI scope and commissioning work affect the quotation. Controller size alone is a poor comparison. Agree additions and exclusions in writing before accepting a price.
Discuss your product or machine with us
Başakşehir Makine is based at İkitelli OSB, Atatürk Blv. Beyaz Tower, Floor 6, No. 90, Başakşehir, Istanbul, Turkey. We agree the scope of on-site work in Istanbul and, for suitable PLC projects across Turkey, remote support or shipment of the controller. For machinery enquiries, samples, delivery and commissioning are agreed in the quotation.
Filling machine options and actual videos · PLC and HMI programming services · Contact us
Manufacturer reference
Siemens S7-1200 G2 online diagnostic and backup tools. This is model-specific documentation; other controllers have different capabilities and access conditions.
The cover is an AI-generated editorial illustration, not a photograph of a delivered customer project or a wiring diagram.